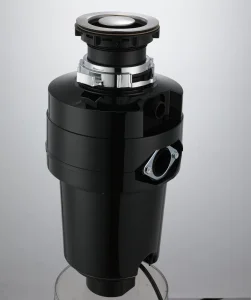
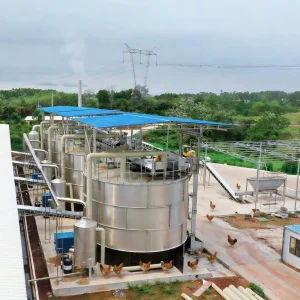
Precision engineered systems engineered for bio-resource conversion, agricultural sustainability, and industrial waste mitigation.
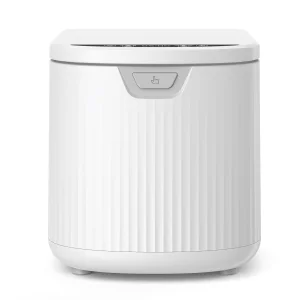
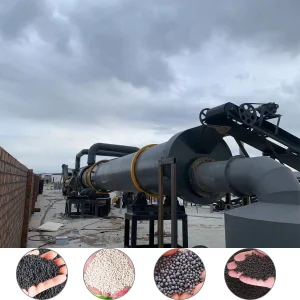
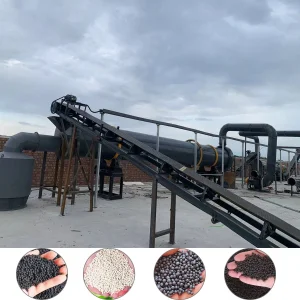
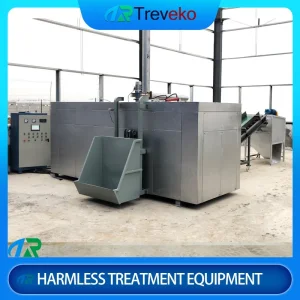
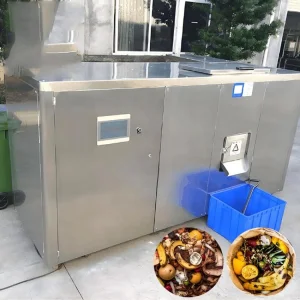
Modern industrial biosecurity, municipal waste reduction goals, and agricultural ESG metrics demand advanced bio-mechanical engineering. Controlled Waste Decomposition Systems (CWDS) represent the convergence of micro-biological kinetic optimization, precise thermodynamic regulation, and automated closed-loop environmental controls. Unlike passive composting or unmonitored incineration, CWDS technologies deliver rapid, pathogen-free, and zero-odor resource recovery.
Integrating hyper-thermophilic bacterial inoculants with controlled thermal feedback loops. Maintaining internal vessel temperatures at 65°C to 75°C rapidly degrades complex biological polymers while completely neutralizing pathogens, weed seeds, and viral strains within 24 to 72 hours.
Equipped with multi-stage negative-pressure air collection, bio-filtration beds, and catalytic oxidation scrubbers. Eliminates ammonia ($NH_3$), hydrogen sulfide ($H_2S$), and volatile organic compounds before atmospheric discharge, ensuring full compliance with stringent urban air quality laws.
Embedded industrial PLC systems monitor moisture dynamic curves, oxygen saturation levels ($O_2 > 10\%$), torque load variables, and mass reduction metrics in real-time. Automated dosing and aeration maximize energy efficiency per metric ton processed.
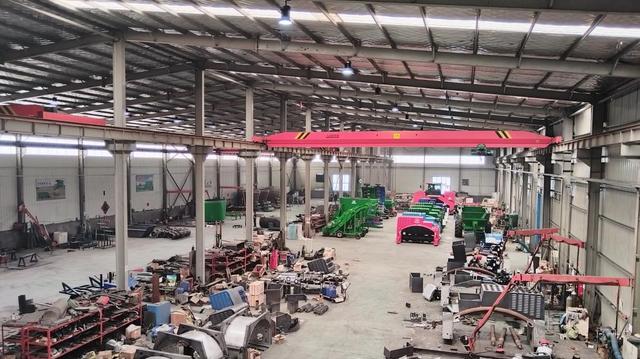
Chengdu AgBio Energy Co., Ltd. is a professional manufacturer specializing in organic waste composting equipment, food waste recycling systems, and sustainable waste treatment solutions. Established in 2013 and headquartered in Chengdu, Sichuan Province, China, the company is dedicated to helping businesses, agricultural operations, municipalities, and environmental service providers transform organic waste into valuable resources. With a modern manufacturing facility covering more than 16,000 square meters and a team of over 230 employees, AgBio Energy delivers efficient and environmentally responsible waste management technologies to customers around the world.
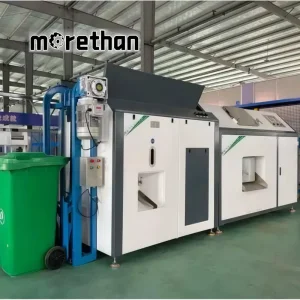
The company's product portfolio includes organic waste composting machines, food waste treatment systems, aerobic fermentation equipment, agricultural waste recycling solutions, manure composting systems, organic fertilizer production lines, municipal bio-waste treatment equipment, and intelligent composting management systems. These solutions are widely used in farms, food processing facilities, restaurants, hotels, commercial waste treatment centers, agricultural cooperatives, and municipal environmental projects.
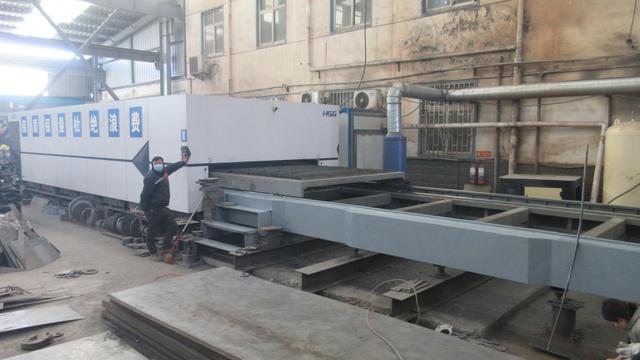
AgBio Energy integrates engineering expertise, process optimization, and advanced manufacturing technologies to develop reliable composting and organic waste recycling systems. The company operates modern production workshops, assembly lines, and testing facilities to ensure product quality, operational efficiency, and long-term reliability. Strict quality management procedures are implemented throughout product development, manufacturing, installation, and customer support processes.
In addition to standard equipment, AgBio Energy offers OEM and ODM services, providing customized waste treatment solutions tailored to specific project requirements, processing capacities, and operational environments. The company works closely with environmental organizations, agricultural enterprises, waste management operators, and project contractors worldwide.
Committed to innovation, sustainability, and resource recovery, Chengdu AgBio Energy Co., Ltd. continues to support global efforts toward circular economy development, landfill reduction, and environmentally responsible organic waste management through advanced composting and recycling technologies.
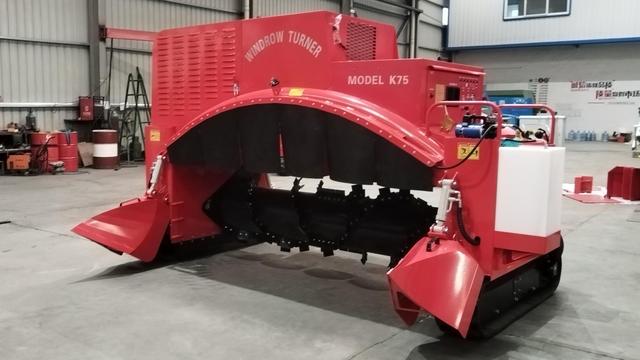
AgBio Energy maintains an aggressive R&D agenda focused on smart automation, carbon-negative processes, and biochemical efficiency enhancements.
Integration of self-learning biological algorithms that dynamically adjust aeration speed, moisture injection, and internal mixing torque based on real-time infrared spectroscopic analysis of organic waste composition. Reduces processing cycles from 24 hours down to 8 hours for municipal food waste streams.
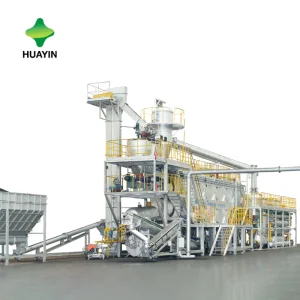
Coupling continuous high-rate aerobic digestion with micro-scale pyrolysis units. Waste heat generated during hyper-thermophilic bio-decomposition is recaptured to pre-dry non-digestible polymer and tire wastes for continuous zero-fuel pyrolysis, yielding bio-char and syngas.
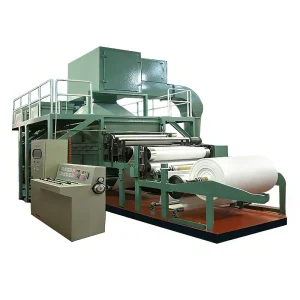
Deploying specialized fungal strain enzyme complexes capable of disintegrating tough fibrous cellulosic matrices, enabling clean bio-pulp production for biodegradable pulp products and toilet paper raw material direct from agricultural crop residues.
Global remote monitoring standard for multi-site municipal facilities. Real-time diagnostic reporting, automated maintenance alerts, micro-climate adaptation, and carbon credit ledger integration verified via immutable blockchain tracking.
Different sector waste streams present unique physical, chemical, and biological challenges. Our engineered solutions target specific industry matrices.
High-moisture animal manure ($80\%+$ water content) requires fast dewatering, ammonia mitigation, and rapid bio-stabilization.
Salt-heavy, oil-rich food scraps demand durable, corrosion-resistant stainless-steel digesters with internal grinding.
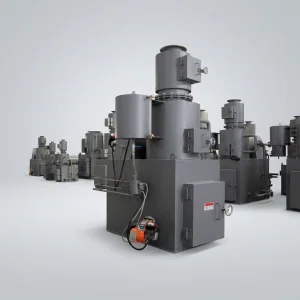
Non-biodegradable hydrocarbon polymers require high-efficiency thermal breakdown and oil extraction processes.
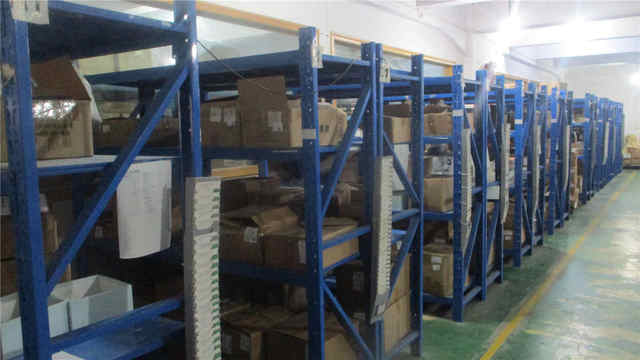
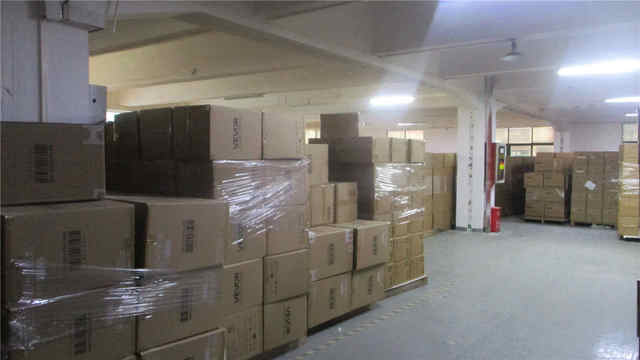
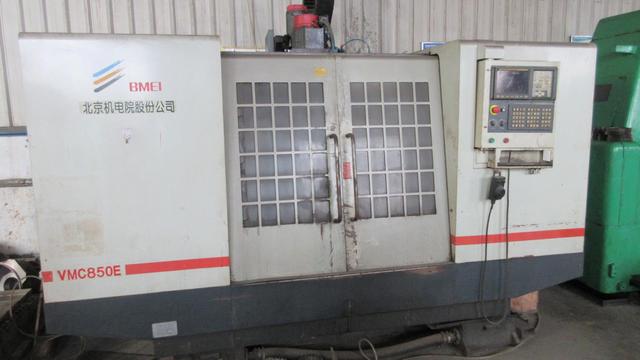
Operating from our 16,000+ $m^2$ facility in Chengdu, AgBio Energy utilizes digital twin engineering, precision robotic welding, and streamlined raw material logistics.
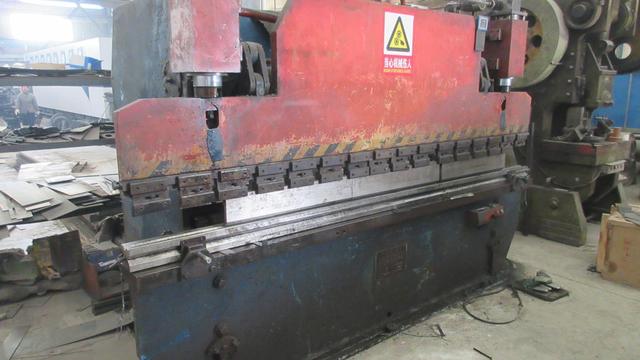
Every reactor tank, agitator shaft, and PLC panel undergoes 72-hour continuous dynamic load testing prior to factory dispatch. Non-destructive ultrasonic welding inspection ensures pressure vessel integrity under harsh operational parameters.
We support complete custom mechanical design—including specialized voltage adaptations (220V/380V/440V/480V), corrosion-resistant SUS304/SUS316 stainless upgrades, custom footprint modular skid designs, and multi-lingual UI panels.
Navigating international cross-border engineering projects requires complete compliance with regional environmental, electrical, and structural safety mandates.
Fully certified for EU CE directives, ISO9001 quality management, ISO14001 environmental management systems, and North American UL/CSA electrical standard options.
Specialized protective coatings and anti-corrosion structural treatments engineered specifically for high humidity, tropical heat, and saline coastal environments across SE Asia (Vietnam, Thailand, Philippines).
Providing remote AR guided assembly, on-site commissioning technicians, extended spare parts inventory dispatch, and bi-annual system optimization audits for international buyers.
Get expert insights into selecting, installing, and maintaining industrial waste decomposition systems.
Specialized machinery engineered for waste-to-energy transformation, bio-pulping, and high-volume municipal resource recovery.
 AgBio Energy