Engineered specifically for Western Uganda's dairy belt, poultry production units, and agro-processing hubs.
A deep technical and commercial analysis for farm owners, agro-processors, municipal contractors, and environmental managers across Western Uganda.
Mbarara City, recognized as the economic engine and agricultural nerve center of Western Uganda, is undergoing rapid transformation. As the primary regional hub for livestock rearing, dairy processing, and high-volume banana (Matooke) cultivation, the municipality generates vast quantities of organic waste daily. Historically, organic management across Mbarara District relied on open dumping, passive lagoon storage, or uncontrolled field spreading. However, heightened regulatory scrutiny by the National Environment Management Authority (NEMA) Uganda, combined with rising commercial land pressures and climate volatility, has rendered traditional disposal methods unsustainable.
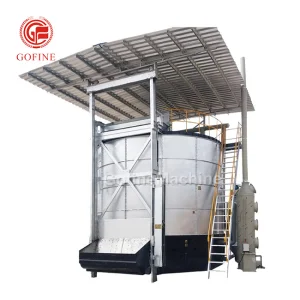
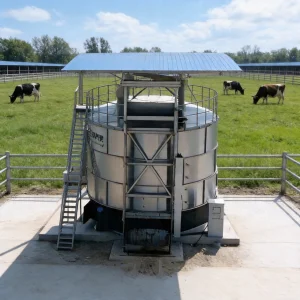
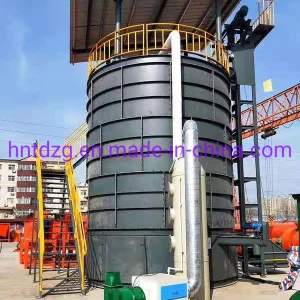
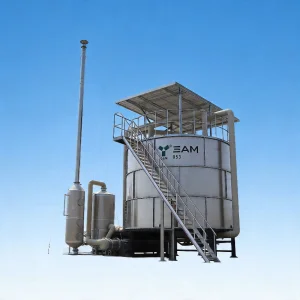
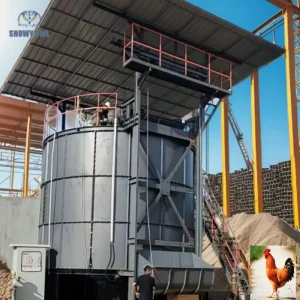
Advanced high-temperature aerobic composting equipment has emerged as the definitive solution for Mbarara’s organic waste challenges. By utilizing forced aeration, precise temperature regulation (60°C–70°C), and automated biological control, modern in-vessel aerobic fermenters convert raw animal manure, food waste, and crop residue into stabilized, bio-secure organic fertilizer within 7 to 15 days. This whitepaper evaluates the structural supply dynamics, technical specifications, return on investment (ROI), and localized deployment strategies for aerobic composting machinery tailored specifically to the climate and operational parameters of Mbarara.
Mbarara serves as the epicenter of Uganda’s dairy corridor. Farms surrounding Biharwe, Kakiika, and Nyakayojo produce metric tons of cattle dung daily. Automated aerobic compost reactors allow large zero-grazing dairy farms to process manure rapidly without odor, eliminating run-off into the Rwizi River catchment area.
The Mbarara central markets and rural collection points produce tons of banana peels, stems, and market garbage daily. Aerobic composting systems enable co-composting high-moisture crop stalks with nitrogen-rich animal manure to create premium soil conditioners for regional horticulture.
For commercial agricultural operators and municipal waste planners in Western Uganda, selecting the appropriate waste conversion asset requires analyzing operational footprint, retention time, pathogen elimination, and nutrient recovery rates. The table below illustrates the stark efficiency differential between legacy open composting/lagoons and modern industrial aerobic equipment supplied by Chengdu AgBio Energy Co., Ltd.
Delivering worldwide-certified biological waste recycling infrastructure from China directly to East African agricultural enterprises.
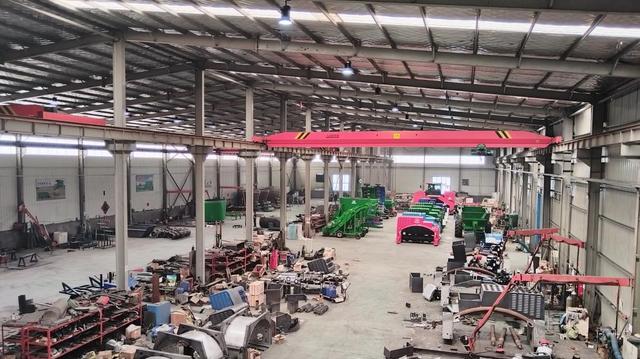
Chengdu AgBio Energy Co., Ltd. is a professional manufacturer specializing in organic waste composting equipment, food waste recycling systems, and sustainable waste treatment solutions. Established in 2013 and headquartered in Chengdu, Sichuan Province, China, the company is dedicated to helping businesses, agricultural operations, municipalities, and environmental service providers transform organic waste into valuable resources. With a modern manufacturing facility covering more than 16,000 square meters and a team of over 230 employees, AgBio Energy delivers efficient and environmentally responsible waste management technologies to customers around the world.
The company's product portfolio includes organic waste composting machines, food waste treatment systems, aerobic fermentation equipment, agricultural waste recycling solutions, manure composting systems, organic fertilizer production lines, municipal bio-waste treatment equipment, and intelligent composting management systems. These solutions are widely used in farms, food processing facilities, restaurants, hotels, commercial waste treatment centers, agricultural cooperatives, and municipal environmental projects.
AgBio Energy integrates engineering expertise, process optimization, and advanced manufacturing technologies to develop reliable composting and organic waste recycling systems. The company operates modern production workshops, assembly lines, and testing facilities to ensure product quality, operational efficiency, and long-term reliability. Strict quality management procedures are implemented throughout product development, manufacturing, installation, and customer support processes.
In addition to standard equipment, AgBio Energy offers OEM and ODM services, providing customized waste treatment solutions tailored to specific project requirements, processing capacities, and operational environments. The company works closely with environmental organizations, agricultural enterprises, waste management operators, and project contractors worldwide.
Committed to innovation, sustainability, and resource recovery, Chengdu AgBio Energy Co., Ltd. continues to support global efforts toward circular economy development, landfill reduction, and environmentally responsible organic waste management through advanced composting and recycling technologies.
We supply customized power configurations (380V/415V 50Hz tailored to Uganda national grid), heavy-duty stainless steel reactors, and complete organic fertilizer granulation lines.
Contact Our Engineering Team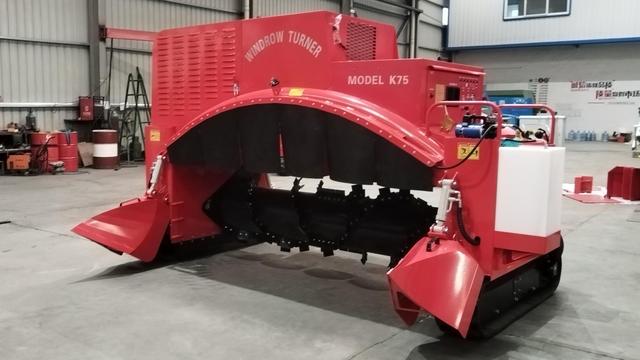
Solving real-world environmental and operational challenges for agricultural and commercial operators in Mbarara.
Mbarara is home to large dairy herds (Ankole and Holstein crossbreeds). Raw slurry management poses severe health risks and odor complaints. Our vertical aerobic tanks ferment manure into sanitized bedding materials or commercial-grade organic fertilizer pellets, generating secondary revenue streams.
High ammonia emissions and moisture content make chicken manure difficult to handle. AgBio's high-temperature aerobic digestion equipment neutralizes ammonia, rapidly evaporates moisture, and destroys harmful pathogens like Salmonella and E. coli in 15 days.
Mbarara Central Market generates tons of biodegradable food waste daily. Integrating our municipal aerobic composting systems diverts up to 70% of organic waste from landfills, extending landfill life and supporting municipal sustainability targets.
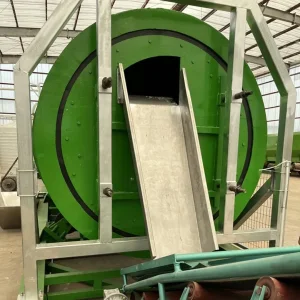
Explore our complete range of specialized aerobic composting reactors, manure dryers, and automated fertilizer production systems.
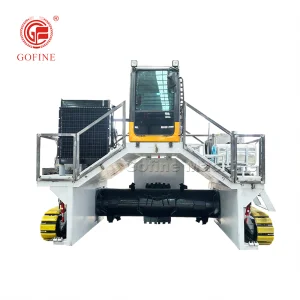
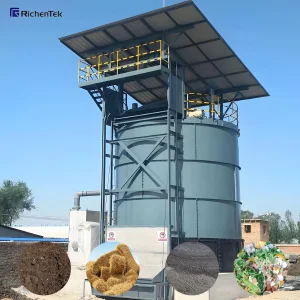
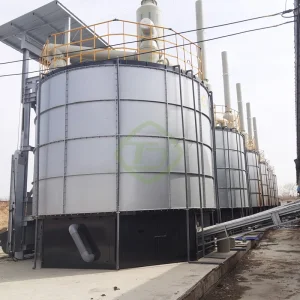
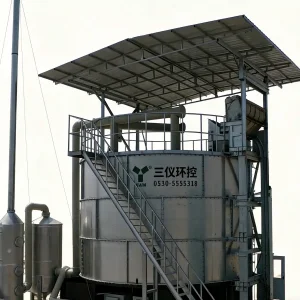
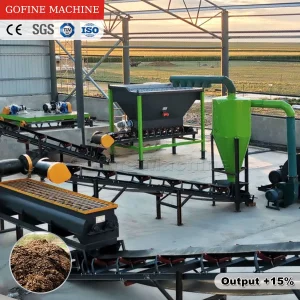
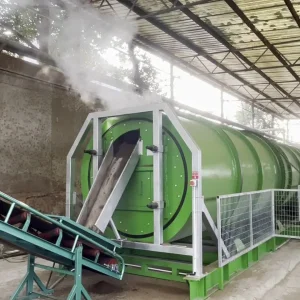
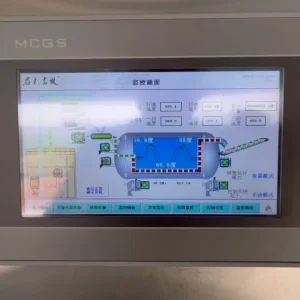
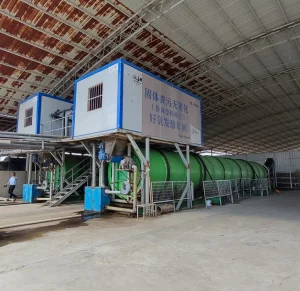
Seamless integration of Chinese manufacturing scale with localized East African operational compliance.
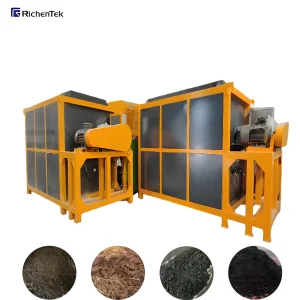
Built with heavy-gauge SUS304/SUS316 stainless steel inner walls and thermal insulation layers, ensuring long operational lifespans under Mbarara’s humid, tropical sub-highland weather condition.
From site layout design and foundation preparation to sea freight dispatching to Mombasa port and road transit directly to Mbarara site, we offer full lifecycle engineering support.
Designed to comply with East African standards for environmental sanitation, biological pathogen elimination, and bio-security, facilitating effortless local authority permitting.
Addressing key technical, logistical, and commercial inquiries regarding aerobic composting equipment deployment.
Get a detailed factory-direct quotation, customized equipment proposal, and engineering ROI assessment today.
Send Inquiry Now AgBio Energy